Home / Metalworking fluids / Metalworking Fluid Sump Management
Field control · Water-miscible fluids

Metalworking Fluid Sump Management

Good chemistry cannot compensate indefinitely for uncontrolled dilution, heavy tramp oil or stagnant zones. Sump management turns a formulation specification into a repeatable operating routine.

OperationOperating machine-tool sump
Fluid familySoluble, semi-synthetic or synthetic
Failure riskOdour, rust, foam, short fluid life
Proof methodTrend chart, inspection and action limits
Formulation target

Define the operating window before selecting chemistry.

The development brief records operation severity, workpiece and tool materials, machine delivery, water or carrier constraints, filtration, downstream processing and the failure that the new product must prevent.

01

Hold concentration inside a validated range

Converted into a measurable screening or field-trial gate.
02

Control tramp oil, chips and stagnant zones

Converted into a measurable screening or field-trial gate.

03

Use simple action limits operators can follow

Converted into a measurable screening or field-trial gate.

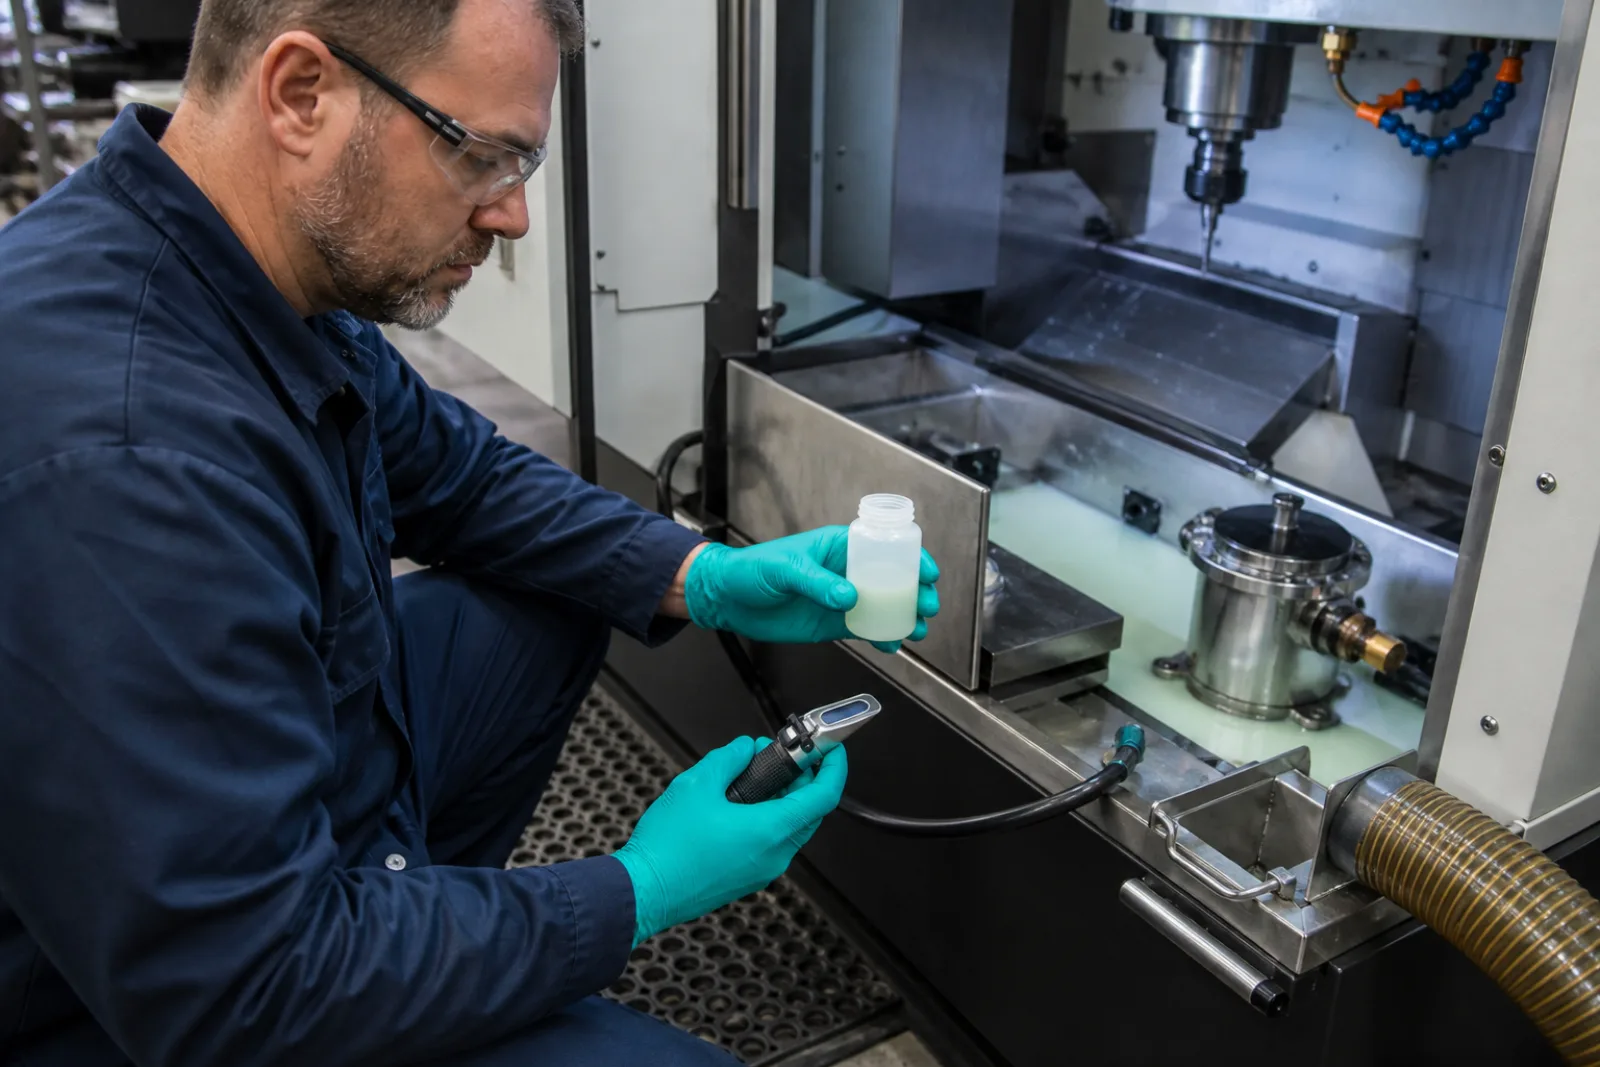
Technician collecting coolant from a machine sump for concentration and condition checks
Trend concentration, pH, appearance and contamination from consistent sampling points; act on movement, not one unexplained number.
Formulation architecture

Build a balanced system, then challenge its weak points.

Raw-material choices are made against the brief, regulatory constraints and available supply routes. Exact components and treat rates remain part of the client-owned development package.

Fluid foundation

Make-up procedure and water-quality control

Performance system

Sampling point, frequency and measurement method

Compatibility control

Tramp-oil removal and filtration routine

Stability support

Escalation, correction and dump/clean criteria

Responsible boundary: this page describes selection logic and evidence gates, not a production recipe. Final composition depends on the client’s raw materials, equipment, safety review, compliance duties and validated trial results.
Qualification gates

Connect each test to a release decision.

A useful programme begins with a baseline, identifies technical risks, screens candidates with appropriate methods and ends with a controlled field trial.

  1. Refractometer calibration and product factor
  2. pH/concentration trend with visual condition
  3. Dip-slide or laboratory microbial trend where appropriate
  4. Tramp oil, fines and foam observation
  5. Corrective-action log and post-action confirmation
Failure map

Diagnose product, process and contamination together.

Falling concentration → inspect leaks, carry-off and make-up
Rising concentration → check evaporation and top-up practice
Odour → remove tramp oil and restore circulation
Foam → find air entrainment before using defoamer
Development handover

What the engagement can produce.

01

Technical brief & risk matrix

Target duties, materials, constraints, acceptance criteria and test plan.

02

Qualified formulation package

Client-owned formula, BOM, manufacturing method and in-process controls.

03

QC specification

Raw-material checks, finished-product limits, sampling and release records.

04

Trial & operating guide

Commissioning, monitoring, corrective actions and change-control notes.

05

Safety and compliance inputs

Data needed for the client’s SDS, label, exposure and market review.

06

Supplier alternatives

Functionally qualified options where substitution risk can be controlled.